Industry News
Curation by industry experts
Hot Articles
Popular Tags
How Do You Verify Industrial Parts Meet Corrosion Resistance Standards?
How Do You Verify Industrial Parts Meet Corrosion Resistance Standards?
How to verify if industrial components meet corrosion resistance standards? Start by separating three things that suppliers often bundle together: the material specification, the protective finish, and the evidence that the finished part meets an agreed requirement. A supplier’s claim or a salt spray duration alone does not establish compliance.
Reliable verification connects the service environment to a suitable specification, then connects the test results to the actual parts being purchased. That last connection is where sourcing decisions often become difficult. A convincing laboratory report may cover a different coating, an earlier production run, or a flat test panel rather than the component in your shipment.
Define the exposure before asking for a test
“Corrosion resistant” is not a complete purchasing requirement. An indoor furniture bracket, an outdoor lighting enclosure, and a fastener exposed to road salt face different conditions. Even within one assembly, sheltered surfaces may retain moisture longer than exposed faces.
Write down the likely exposure: indoor humidity, condensation, coastal chlorides, cleaning chemicals, temperature changes, or intermittent immersion. Include contact with other metals. A stainless steel screw in an aluminum housing creates a different assessment from the same screw installed in a compatible stainless assembly, particularly when an electrolyte is present.
Also decide what failure means. Is cosmetic staining unacceptable, or is the concern loss of section, seized threads, coating delamination, or water entering an enclosure? A decorative component may fail appearance requirements before its structural function is affected. A threaded component can look acceptable while corrosion compromises removal or adjustment.
Without these decisions, suppliers may quote entirely different protection systems against the same vague request.
Use the right standard—and understand what it does not specify
ASTM B117 and ISO 9227 are widely used references for salt spray testing. They describe controlled test conditions and procedures; they do not, by themselves, provide a universal pass requirement for every industrial part. A statement such as “ASTM B117 compliant” therefore needs clarification: which product requirement was evaluated, for how long, and against what acceptance criteria?
ISO 9227 covers neutral salt spray, acetic acid salt spray, and copper-accelerated acetic acid salt spray methods. These are not interchangeable labels. The selected method must suit the coating system and the governing specification. Likewise, results under ASTM B117 and ISO 9227 should not automatically be treated as contractually equivalent.
The material or finish specification supplies another part of the answer. For example, ASTM F1941/F1941M addresses electrodeposited coatings on mechanical fasteners, while ISO 10683 addresses non-electrolytically applied zinc flake coating systems for steel fasteners. ISO 12944 is relevant to protective paint systems for steel structures, not a blanket approval standard for every painted component.
Confirm the applicable edition and product scope before putting a standard on a purchase order. Where an OEM specification or sector-specific qualification applies, use its prescribed sequence rather than substituting a familiar salt spray test.
Turn the requirement into an inspectable statement
A usable requirement identifies the substrate, coating designation, relevant thickness limits, test method, exposure duration, and permitted deterioration. It should also define significant surfaces, sample quantity, and treatment of edges, threads, recesses, and intentional scribes.
Do not insert an arbitrary number of hours simply because competitors advertise it. Select the exposure and acceptance criteria from the applicable product specification or an engineering-approved validation plan.
Read the report as evidence, not as a certificate
Begin with sample identity. The report should identify the tested component, drawing revision where relevant, material, finish, and a lot or sample reference that can be connected to production records. If the supplier sells several finishes under one commercial name, insist on the actual coating designation.
Then examine how the test was performed. Useful reports record the method and edition, exposure conditions and duration, specimen preparation, orientation, inspection intervals, and deviations. Photographs should correspond to identified specimens and show the areas used for evaluation.
- Check the stated outcome. “Test completed” is not the same as “acceptance criteria met.” Look for observations and an explicit basis for the conclusion.
- Separate corrosion types. White corrosion products on a zinc-based finish and red rust from the steel substrate are different observations. Whether either is acceptable depends on the specification.
- Look for exclusions. Masked surfaces, cut edges, contact marks, and unassessed recesses can materially limit what a result proves.
- Check report authenticity. If details are inconsistent, verify the report number with the issuing laboratory through independently confirmed contact information.
An ISO/IEC 17025-accredited laboratory can provide stronger confidence in testing competence, but review its accreditation scope. Accreditation for unrelated tests does not establish competence for the corrosion method you need. Nor does an accredited report automatically qualify a supplier’s entire product range.
An older report is not necessarily invalid. The practical question is whether it still represents the current material, coating process, manufacturing location, and part geometry. A recent date cannot compensate for the wrong sample.
Inspect the part where the coating is most vulnerable
Flat test panels are useful for controlling a finishing process, but they cannot reproduce every weakness in a manufactured component. Sharp edges, punched holes, welds, deep recesses, and handling points can behave differently from broad, accessible surfaces.
Consider a powder-coated outdoor lighting bracket. A panel may demonstrate that the coating system performs under the specified exposure, yet say little about coverage inside the bracket’s folded return or around a mounting slot. Those details need examination on representative finished parts.
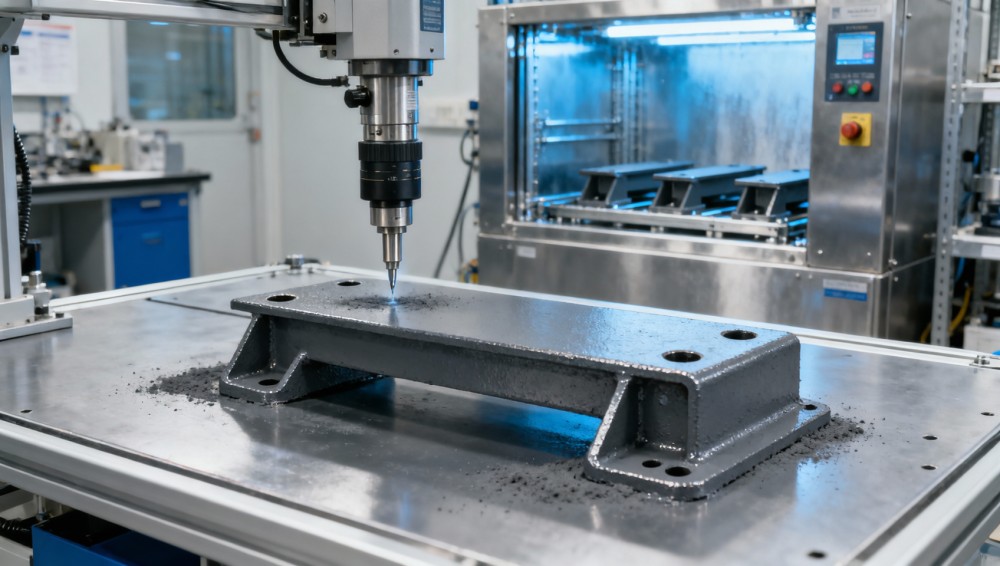
Check coating thickness using a method suitable for the substrate, coating, and geometry. Magnetic or eddy-current instruments are useful in appropriate applications; X-ray fluorescence or cross-sectional examination may be more suitable for certain metallic layers. Measurement location, calibration, curvature, and access all affect interpretation. One reading on an easy-to-reach face is rarely enough.
Thickness alone is not proof of protection. Poor surface preparation, inadequate curing, porosity, or weak adhesion can undermine an apparently adequate coating. Add adhesion or other process checks where the finish specification requires them. For stainless parts, verify the specified alloy and any required cleaning or passivation treatment; a shiny surface is not evidence of either.
Inspect after relevant manufacturing steps. Bending, welding, thread forming, assembly, and installation can damage a previously acceptable finish. The qualification sample should represent the condition in which protection is actually needed.
Do not convert salt spray hours into service years
A longer accelerated test result does not establish a proportional increase in outdoor life. Continuous salt fog differs from real exposure, which may include drying, sunlight, contaminants, temperature cycling, and maintenance. Some protective systems depend on surface films that develop differently under laboratory and field conditions.
Salt spray testing is valuable for checking consistency and assessing conformance to a defined requirement. It is much less defensible as a universal ranking tool across unrelated materials and coatings.
Where wet-and-dry cycling or other combined stresses drive failure, a specified cyclic corrosion method may be more relevant. Painted outdoor products may also need separate evaluation of weathering and adhesion. Components in chemical service may require exposure testing against the actual fluid at the relevant concentration and temperature. These tests answer different questions; they are not upgrades that can be substituted without engineering review.
Connect qualification to the shipment you receive
A successful qualification establishes evidence for a defined product and process. Routine purchasing still needs controls that keep subsequent production within that definition.
Request a traceable documentation package appropriate to the risk: material records, coating batch references, inspection results, and the relevant qualification report. A certificate of conformity should cite the agreed requirements, but it remains a declaration—not a replacement for supporting records.
Use a documented sampling plan that reflects component criticality, process history, and contractual obligations. Destructive corrosion testing of every delivery may be impractical. Periodic validation combined with routine thickness checks, visual inspection, and process monitoring may be appropriate, provided the governing specification permits that approach.
Require notification before changes to the coating chemistry, pretreatment, applicator, substrate, or manufacturing route. Depending on the change, existing qualification evidence may need review or repeat testing. Also inspect packaging and storage conditions: condensation or trapped moisture can damage otherwise conforming parts before installation.
For cross-category sourcing covered by Global Supply Review (GSR)—including hardware, lighting, and furniture components—the useful comparison is not the largest advertised salt spray number. It is whether competing suppliers provide equivalent, traceable evidence against the same requirement.
Before releasing an order, resolve three questions: what must pass, which evidence proves it, and how that evidence connects to the delivered lot. If any answer is missing, clarify the requirement before shipment rather than treating an impressive-looking report as approval.
Recommended News
 Supply Chain InsightsHow to use supply chain resilience metrics to assess recovery riskUse supply chain resilience metrics to compare recovery time, survival buffers, and financial exposure. Learn how to assess disruption risk and prioritize mitigation that protects service.Oct 18, 2026
 Commercial LEDHow to assess an LED street light exporter’s warranty coverageAssess an led street lights exporter beyond warranty length. Learn how to verify coverage, uncover hidden costs, and negotiate stronger terms before you buy.Commercial Tech EditorOct 17, 2026
 Carton & PlasticsWhen should you heat seal aluminum foil zipper bags for food storage?When should you heat seal aluminum foil zipper bags? Learn when stronger closures matter, how to protect dry foods, and which sealing checks help ensure reliable storage.Packaging Supply ExpertOct 16, 2026
 Supply Chain InsightsHow to find a custom-printed ring-pull can supplier for small ordersFind a custom printed ring pull cans supplier for small orders. Compare MOQs, printing options, samples, and delivered costs to launch confidently without excess inventory.Oct 15, 2026