Industry News
Curation by industry experts
Hot Articles
Popular Tags
How to assess a flat bottom pouch supplier’s quality controls
Assess the control system before you assess the samples
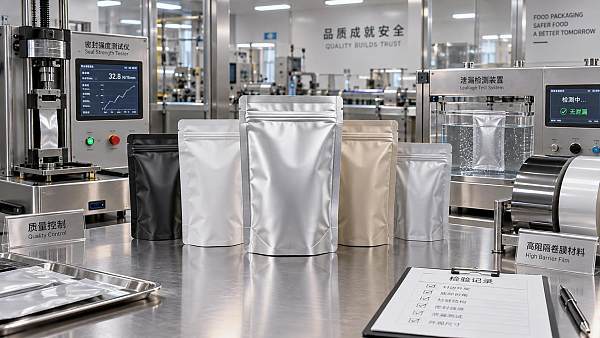
A flat bottom pouch can look acceptable on a desk and still create failures on a packing line, in distribution, or after filling. The format has more panels, more formed edges, and more sealing interfaces than a simple three-side pouch. That makes consistency especially important. A supplier should be assessed on whether it can control repeatability across material conversion, printing, pouch forming, and release inspection, not simply on whether it can produce one attractive sample.
For quality and safety teams, the most useful starting question is: can this supplier show how it prevents defects, detects them when prevention fails, and traces affected production when an issue reaches the customer? A capable flat bottom pouch supplier will answer with documented controls, defined acceptance criteria, retained records, and people who can explain how those elements work together. General statements about “strict quality” or “advanced equipment” do not answer that question.
Assessment should concentrate on four connected areas: material and compliance control, critical pouch performance, process discipline, and release traceability. Weakness in one area can undermine the others. Good film specifications cannot compensate for poorly controlled seals; a sound final inspection plan cannot fully correct a process with unstable web tension or inconsistent sealing conditions.
Start with the pouch’s actual use conditions
Before auditing a supplier, translate the intended application into a practical risk profile. A pouch for dry snacks, coffee, powdered ingredients, pet food, detergent, or industrial granules may share the same broad format, but the control points are not identical. Product weight, particle shape, oil content, filling temperature, oxygen sensitivity, storage humidity, shipping route, and consumer opening behavior can all change the acceptance standard.
For example, a pouch carrying sharp or abrasive contents needs confidence in puncture resistance and gusset integrity. A product with aroma or oxidation sensitivity raises the importance of barrier structure and seal integrity. A pouch used for a food-contact application requires a clearer view of raw-material declarations, migration-related documentation where applicable, ink and adhesive suitability, and controls against contamination. A high-gloss retail pack may place greater emphasis on print registration and rub resistance, but appearance should not displace functional testing.
This application definition should become the basis of the supplier brief. It should state the pouch dimensions and tolerances, filling weight, intended filling and sealing equipment, product-contact requirements, barrier needs, closure type, artwork version control, carton configuration, and conditions expected in transport and storage. Without this baseline, a supplier may offer standard test reports that are technically valid but irrelevant to the failure modes that matter.
Ask for a control plan tied to critical characteristics
The supplier’s control plan is more revealing than a generic quality manual. It should identify the characteristics considered critical, where they are checked, how often they are checked, the measurement method, acceptable limits, responsibility for the check, and actions when results fall outside the limit.
For flat bottom pouches, critical characteristics commonly include:
- Film, foil, paper, adhesive, ink, zipper, valve, and other component identification against the approved specification.
- Finished dimensions, including width, height, bottom panel, side gusset, and alignment of formed panels.
- Seal width, seal appearance, seal strength, and continuity around the bottom and vertical structures.
- Leak performance under a method appropriate to the product and pack design.
- Print registration, color approval process, legibility of variable information, and artwork revision control.
- Barrier-related properties when the product specification depends on them.
- Foreign-material and hygiene controls for product-contact packaging.
- Finished-roll or finished-pouch identification, packing integrity, and shipment release status.
A supplier does not need to use the buyer’s terminology, but it should be able to demonstrate the same discipline. If it cannot explain which characteristics are safety-critical, functional, or cosmetic, inspection may be driven by what is easiest to observe rather than by what is most likely to cause a market complaint.
Examine material control beyond certificates
Certificates and declarations are useful, but they are only one part of material control. Buyers should understand how the supplier prevents the wrong substrate, adhesive, ink, zipper, or barrier layer from entering an approved order. This is particularly important where similar films are stored together, multiple material structures are converted on the same site, or the pouch is made from laminated webs supplied by outside converters.
During an assessment, look for a clear receiving process: supplier approval, incoming identification, status labeling, storage conditions, inspection or verification requirements, and a method for handling nonconforming materials. Material lots should remain linked to production lots. If an issue is found later, the supplier needs to identify both the affected finished pouches and the source materials used in them.
For food, beverage, pharmaceutical-adjacent, or sensitive consumer applications, ask how product-contact suitability is controlled through change management. A declaration issued for one material structure should not be treated as a blanket approval for a visually similar substitute. Changes in resin grade, ink system, adhesive, coating, recycled-content source, or subcontracted conversion can alter risk even when the pouch’s external appearance remains unchanged.
The same concern applies to sustainability claims. Recyclable, compostable, recycled-content, and reduced-material structures can bring different processing windows and mechanical behavior. A supplier should be able to distinguish an approved material claim from an approved functional specification. A change made to support an environmental target still needs seal, barrier, migration-related, and line-performance review where relevant.
Questions that expose weak material governance
- Can the supplier trace a finished pouch batch back to every major material lot?
- What prevents an unapproved substitute from being issued to production?
- Who authorizes a material or process change, and how is the buyer informed when prior approval is required?
- How are expiry-sensitive materials, such as certain adhesives or inks, controlled in storage and at point of use?
- Which documents are reviewed before a new material structure is released for production?
- When components are purchased from external converters, what incoming verification is performed rather than assumed?
An answer that relies only on supplier certificates, without a site-level segregation and traceability process, leaves a meaningful gap. Paperwork can establish a starting point; operational control establishes whether the right material was actually used.
Test the features most likely to fail in service
Seal integrity deserves special attention. Flat bottom pouches combine longitudinal, transverse, bottom, and gusset-related sealing zones. Seal quality can be affected by temperature, pressure, dwell time, jaw condition, film variability, contamination in the seal area, web alignment, and pouch geometry. A supplier should define its validated or established operating windows and monitor the parameters that influence the seal.
Do not accept a statement that seal strength is “tested regularly” without asking what that means. The relevant questions are where samples are taken, whether all critical seal areas are represented, how results are recorded, and what happens after a failure. A single test strip from an easy-to-access area may not represent the most stressed portion of the pouch. For a pouch that must stand upright, the bottom formation and corners require particular scrutiny because defects there may show only when the pack is filled.
Leak testing should also reflect the intended pack. Methods may differ, but the supplier should have a documented rationale for the chosen method and acceptance criteria. A visual check is useful for obvious defects, yet it is not a sufficient substitute for a controlled integrity test where leakage can compromise product safety, shelf life, or containment. If the pouch will hold powders, fine particles, liquids, or volatile products, agree on the performance requirement before commercial production.
Print control is often treated as a lower-risk area, although artwork mistakes can trigger costly holds or recalls. Review how the supplier manages approved artwork files, plates or digital print data, color standards, barcode or code legibility where used, and line clearance between jobs. The central risk is not only color variation. It is the possibility that an obsolete design, incorrect declaration, wrong language version, or mismatched component is released into production.
For packs with zippers, valves, handles, tear notches, laser scoring, or resealable features, request evidence that these additions are inspected as functional components. A zipper can appear correctly positioned while failing to engage consistently. A tear feature can open prematurely or fail to initiate. Each feature introduces a separate potential failure mode and should have a specific acceptance criterion rather than being covered by a general visual inspection.
Audit the production floor for discipline, not presentation
A well-organized facility is encouraging, but a quality assessment should follow the product path. Observe receiving, storage, slitting or printing where applicable, lamination or curing where applicable, pouch making, inspection, packing, quarantine, and dispatch. Look for evidence that product status is visible and that nonconforming material cannot drift back into approved stock.
Control of setup and changeover is especially important. The supplier should be able to show how it verifies the correct material structure, artwork, dimensions, and forming settings before a run begins. First-off approval should be more than a signature on a form. It should confirm the features that are vulnerable to a wrong setup: pouch geometry, seals, print version, registration, zipper or valve placement, and pack identification.
In-process checks should be conducted at a frequency that matches the stability and risk of the operation. A schedule that is fixed only by time may miss a defect arising after a roll splice, material change, machine adjustment, or restart. Better systems connect additional checks to events that can affect quality. Ask whether operators record machine interventions and whether the product made since the last acceptable check is placed on hold when a critical defect is found.
There should also be a credible nonconformance process. Inspect the physical controls as well as the procedure: marked quarantine locations, labels that identify the reason for hold, restricted disposition authority, rework rules, and records of final disposition. Rework must be tightly controlled for packaging intended for sensitive applications. A supplier that cannot show how suspect material is contained may be unable to limit the scope of a later investigation.
Look for corrective action evidence
Every manufacturer has occasional defects. The distinction lies in how it responds. Ask for anonymized examples of corrective-action records related to pouch defects, print errors, or material discrepancies. The useful evidence is not the incident itself but the quality of the investigation: identification of the affected lot, immediate containment, root-cause analysis, corrective action, verification of effectiveness, and communication to customers where required.
Be cautious when all examples end with operator retraining. Training may be appropriate, but recurring problems often point to a missing process control, unclear specification, inadequate maintenance, poor changeover verification, or unsuitable inspection method. A robust system identifies the condition that allowed the error and changes that condition.
Traceability and release should support a realistic recall scenario
Traceability is sometimes assessed as an administrative requirement. For a packaging supplier, it is a risk-containment tool. The supplier should be able to retrieve the production record for a finished batch and connect it to material lots, production date and shift, equipment, inspection records, artwork version, rework status where allowed, packing details, and shipping destination.
Ask the supplier to walk through a mock exercise: a defect is identified in an approved material lot after shipment. How would it identify affected pouch batches, inventory still on site, shipments already dispatched, and any related production runs? The response should be based on records, not a verbal assurance that its enterprise system can provide the information. Manual systems can work if they are complete, legible, secure, and routinely reconciled; digital systems can fail if users bypass them.
Finished-goods release is the final barrier before shipment. Establish who has authority to release a batch, what records must be complete, how deviations are reviewed, and whether samples are retained for investigation. The release process should prevent commercial urgency from overriding incomplete checks. That question matters most when the supplier operates short lead times or handles frequent artwork changes.
Use pre-production approval to validate the supplier’s controls
A site audit and document review should be followed by a controlled pre-production stage for new suppliers, new structures, or high-risk applications. The objective is to confirm that the agreed specification can be made consistently under normal operating conditions, not to obtain a hand-finished prototype.
Agree in advance on the approval package. It may include approved artwork, material structure, dimensional tolerances, test methods, visual standards, relevant declarations, sampling rules, batch coding requirements, and criteria for handling deviations. Where practical, run the pouch on the buyer’s filling line or under representative filling conditions. Problems such as poor machine handling, inadequate stiffness, seal contamination, poor opening behavior, or unstable standing performance often emerge only after the pouch enters its intended process.
Commercial approval should remain conditional on the supplier maintaining the approved structure and control plan. A sample approval without formal change notification terms can create a false sense of security. The most reliable supplier relationship is one in which changes are visible early, documented clearly, and reviewed according to their likely impact on safety, compliance, function, and appearance.
Make the supplier decision evidence-based
Price, capacity, and lead time still matter, but they should be evaluated after the supplier has demonstrated control of the risks that a flat bottom pouch can introduce. A lower-cost source may create a much higher exposure when batch segregation is weak, sealing records are incomplete, material changes are informal, or release authority is unclear.
For quality and safety teams, the decision is rarely about finding a supplier with the longest certificate list. It is about selecting one whose documented system is visible on the production floor and whose records can withstand a defect investigation. When material identity, seal performance, artwork governance, nonconformance containment, and traceability are all controlled as one process, the supplier is far better positioned to produce pouches that remain reliable beyond the sample stage.
Recommended News
 Carton & PlasticsWhen do double wall corrugated boxes prevent damage in transit?Double wall corrugated boxes prevent transit damage from stacking, impact, punctures, and long-haul handling. Learn when stronger packaging delivers smarter protection.Packaging Supply ExpertSep 14, 2026
 Carton & PlasticsHow to assess a flat bottom pouch supplier’s quality controlsFlat bottom pouch supplier quality controls: assess materials, seal integrity, traceability, change management, and release processes to reduce packaging risk.Packaging Supply ExpertSep 13, 2026
 Office FurnitureHow to compare wholesale commercial carpet tiles by installed costCommercial carpet tiles wholesale: compare installed costs, freight, waste, subfloor prep, labor, and lifecycle value to make smarter procurement decisions.Interior Sourcing LeadSep 12, 2026
 Carton & PlasticsWhen is 200 gsm kraft liner board strong enough for shipping cartons?Kraft liner board gsm 200: learn when it delivers reliable carton strength, how flute, stacking, moisture, and box size affect performance.Packaging Supply ExpertSep 11, 2026